-
By Pieter
-
November 20, 2026
- 0 Comment
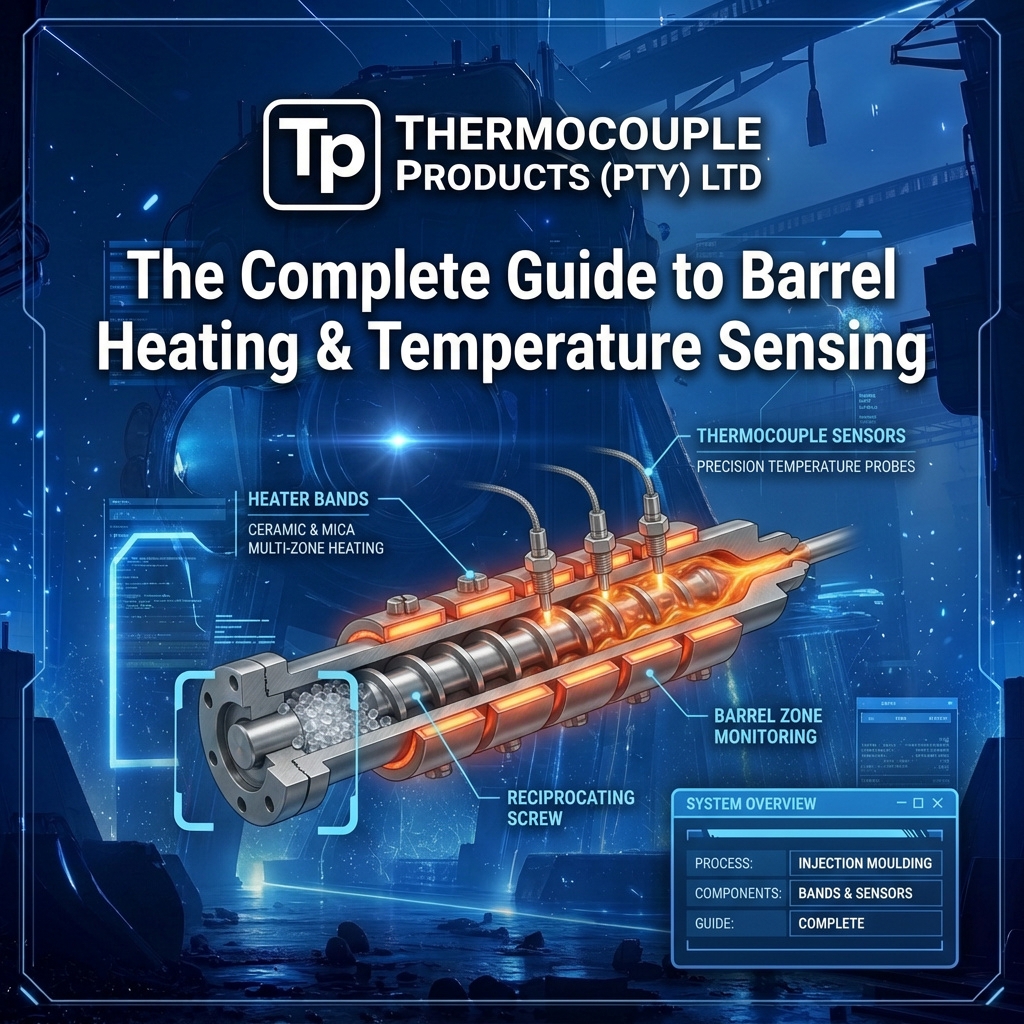
The Complete Guide to Barrel Heating and Temperature Sensing on an Injection Moulding Machine
The Complete Guide to Barrel Heating and Temperature Sensing on an Injection Moulding Machine
The short answer: A moulding machine barrel is heated by band heaters clamped around it and measured by a thermocouple or Pt100 inserted into the barrel near each zone. The reading drives the controller, the controller drives the band, and the melt gets whatever the loop produces. When the parts disagree with the display, the cause is almost always one of five things — sensor depth and position, heat conducted away up the sheath, poor band contact, junction type and earth loops, or the extension cable between.
This is the first of four guides on plastics processing: the barrel this week, then the hot half, the mould and cooling, and finally uptime and spares. It assumes you know what a barrel is. That is the point.
Thermocouple Products manufactures thermocouples, Pt100 RTDs and industrial heating elements in Edenvale, Gauteng — including the band heaters on the barrel, the cartridge and supercoil heaters in the tool, and every sensor in between. That combination is why this guide can cover the whole thermal system rather than one component of it.
Why the barrel is a temperature profile, not a temperature
The single most useful idea in injection moulding from a thermal point of view: the barrel is not set to a temperature. It is set to a profile.
A typical barrel carries four to six heated zones between the feed throat and the nozzle, and they are deliberately set at different temperatures:
- Rear zones, lower. Resin entering the rear of the barrel is being conveyed and compressed by the screw. It needs to soften and to grip the barrel wall so it can be conveyed forward. Soften it too early and it slips on the screw instead of moving — the screw turns, nothing feeds, and everyone blames the machine.
- Middle zones, rising. This is where melting properly happens, and most of the energy comes from shearing work done by the screw rather than from the band heaters. The bands maintain what the screw achieves.
- Front zone and nozzle end, hottest. The melt must arrive fully prepared and homogeneous, ready to be injected in a fraction of a second.
Which means a zone that reads a few degrees wrong is not a cosmetic problem. It silently changes a profile that someone chose deliberately for a specific material and a specific part — and the resulting defects (short shots, flash, sink, weld lines, dimensional drift) get investigated as moulding problems when the root cause is a thermometer.
If your process window is being widened to make parts, check the temperature measurement before checking the tool.
How the barrel is heated
Band heaters clamp around the barrel and heat by conduction — the band’s inner surface must sit in tight, even contact with the barrel along its whole width. That single sentence governs most band heater behaviour.
Mica band heaters are the workhorse of the barrel: Nichrome resistance wire or ribbon wound inside mica insulation, in a stainless or aluminised steel sheath, with a clamping system to close it around the barrel. They typically run at a watt density of 3 to 7 W/cm² (20 to 45 W/in²) and are rated to about 480°C.
Ceramic band heaters use ceramic insulation with a ceramic fibre blanket, rated continuously to 760°C, and the insulation reduces heat loss by roughly 25% to 30% compared with an uninsulated equivalent — lowering the external sheath temperature and the load on factory cooling as well as saving power.
For the overwhelming majority of moulding work — engineering and commodity resins alike — mica is the correct and economical choice. Ceramic earns its cost where the barrel genuinely runs hotter, or where the heat-loss saving and surface temperature matter in a hot workshop.
On the barrel, watt density is the number to watch. A band with too little wattage for its zone will struggle to hold set point and will spend its life at 100% output; a band with too much will overshoot, cycle hard and fail early. Both look like “a bad heater” from the shop floor, and neither is.
What a band heater’s failure tells you
- Localised burnt or blistered patch — poor contact at that spot, or a hot spot on the barrel. A fit problem, not a manufacturing one.
- Even discoloration and ageing over the whole band — normal end of life.
- Failed clamp or distorted body — usually a band that was opened out, flattened or forced onto a barrel it was not made for. Bands are sized to a specific outside diameter, and a distorted one can never sit properly again.
- Burnt leads near the terminal — lead temperature or mechanical damage, often from a cable routed against a hot surface.
If the same zone kills a band twice in the same way, stop ordering bands. The third one will fail exactly like the first two. See the five causes below.
How the barrel thermocouple is installed
Barrel temperature is measured by a thermocouple or Pt100 in a hole drilled into the barrel wall, close to but rarely touching the melt. It reads the steel around it — and the relationship between that steel and the plastic is what the whole control loop depends on.
Three installation details matter more than the sensor’s specification:
Depth and seating. The sensor must be fully home in a clean, properly drilled hole, at a consistent depth relative to the zone it controls. A sensor sitting proud of the hole, or in a hole partly filled with swarf or hardened resin, reads the barrel surface where the heater’s influence is strongest rather than the barrel body.
Contact and fit. A loose sensor in an oversized hole is surrounded by an air gap, and still air is an excellent insulator. Response slows, the reading lags the zone, and the controller compensates by overshooting and cycling harder.
Sheath mass. This is the effect almost nobody accounts for, and it deserves its own section.
Heat travelling up the sheath: the invisible cause
A thermocouple in a barrel hole is a metal rod in a hot block with one end sticking out into workshop air.
Heat does not only flow from the barrel into the sensor. It also flows along the sensor, out of the barrel, and into the ambient air — because the exposed length of a stainless sheath conducts very effectively and radiates and convects heat away once it is outside the block.
A long, heavy sheath in a deep hole therefore reads a cooler average than the zone it is measuring. Not because it is faulty, and not because it is miscalibrated: because the geometry conducts heat away from the measuring junction.
The practical consequences:
- The error is consistent and stable — a few degrees low, every day. That is what makes it so hard to spot: nothing looks wrong.
- It scales with exposed length and sheath mass. A sensor with 100 mm sticking out into moving cool air loses more than a compact assembly tucked in close.
- It is worse in a cold workshop with air movement — which describes most factories in winter.
What reduces it: a slim mineral insulated sensor, a well-fitted hole, and as little exposed length of sheath as the installation allows. MI construction is particularly effective here — its sheath is small in diameter and the compacted magnesium oxide holds the conductors close to the sheath wall, so response is fast and the conduction path up the sheath carries less heat away relative to its length.
If a zone has always read a little low, and the reading has always been stable, this is worth considering before anything is replaced.
The five causes of a wrong barrel reading
In order, check the cheapest first.
1. The sensor is not deep enough, or not in the right place
Fully home? Hole clean? Same depth as the zone it controls? A shallow or poorly seated sensor measures the wrong part of the barrel, and no amount of controller tuning fixes a measurement taken in the wrong place.
2. Heat is being conducted away up the sheath
Covered above. Consistent, stable, slightly low, worse in cold air. Solve with a slim MI sensor, a fitted hole and minimal exposed sheath.
3. A band heater problem is presenting as a sensor problem
A loose, distorted or scaled band creates a local hot spot. The sensor reads the average; the controller controls the average; a patch of barrel cooks. Everyone concludes the sensor is “slow” or “lagging”.
Look at the band’s fit and clamping, and at where any damage on the old band sits. Localised damage is a contact problem.
4. Wrong junction type, or a noisy electrical loop
A grounded (G) junction is welded to the sheath tip: fastest response, no electrical isolation. On a machine with variable frequency drives, switching contactors and heater loads, that missing isolation becomes earth loops, and earth loops appear as readings that wander, jump or never quite settle.
An ungrounded (U) junction is isolated from the sheath. It responds more slowly but eliminates a very large category of instability. On a busy moulding machine it is the sensible default, and if one zone has been jumpy for years, this is a strong candidate.
An exposed (E) junction exists where speed matters most and the medium is benign; it is rarely the right choice in a barrel.
5. The cable between the sensor and the controller
The wrong extension cable for the thermocouple type, a reversed connection, or a run routed alongside power conductors can each produce a fixed offset or an erratic signal from a perfectly serviceable sensor.
It is the cheapest of the five to check, which is why it should be checked earlier than its position on this list suggests.
The diagnostic shortcut
- Stable, believable, slightly low → geometry (depth, fit, sheath conduction) or cable.
- Unstable, jumpy, wandering → electrical (junction type, earthing, cable routing).
- Correct at set point but the parts behave otherwise → the melt, the screw, or the tool — the measurement may be telling the truth.
Sensors rarely fail politely. A sensor that has “slowly gone a bit wrong” while remaining perfectly stable is usually not a sensor at all.
Zones that will not hold temperature
A zone that sits below set point and will not climb is one of the most common calls in a moulding shop. The cause is usually one of these:
Symptom | Likely cause | Check |
Below set point, output at 100% | Band wattage too low for the zone, or a band failing | Band rating against duty; measure the current drawn |
Below set point, band cold | Failed band, failed thermocouple, wiring, or controller output | Thermocouple reading in an ice bath; continuity; controller output |
Reaches set point, then falls away | Intermittent connection, failing band, or thermocouple intermittently open | Wiggle test on leads; inspect terminals |
Overshoots and cycles hard | Watt density too high, sensor lag, or poor tuning | Band rating; sensor fit and depth; PID settings |
One zone behaves unlike its neighbours | Local fault on that zone only — fit, sensor, band or wiring | Compare with an adjacent zone’s behaviour |
Reads wildly different from a handheld check | Sensor or installation problem | Handheld comparison at the barrel surface |
The rule that saves the most time: compare the misbehaving zone with its neighbours. Machine, product, controller and operator are common to every zone, so whatever differs is local — and that halves the search immediately.
The other zones on the machine
The barrel is the largest thermal system on a moulding machine, not the only one. In brief, and covered in the following weeks of this series:
Hot runner manifold — heated by cartridge heaters, because the geometry is a drilled block rather than a cylinder. High watt density, fully localised, often several zones on one manifold. (Week 14.)
Hot runner nozzles — supercoil heaters, around 4,2 mm × 2,2 mm, in a space too small for anything else, frequently built with their own type J or K thermocouple inside the assembly. The smallest heaters in the plant, in the hardest place to reach.
Feed throat — usually cooled, not heated. A hot feed throat makes resin stick and bridge before it reaches the screw. If the throat is warm, that is a cooling problem, and no heater will solve it.
Mould and cooling — the tool’s temperature is a thermal system of its own, with its own sensors.
The spare list for a machine you cannot stop
Deep-diving one machine makes one commercial point obvious: a small, deliberate set of spares converts a two-day breakdown into a two-hour one.
Band heaters
- One spare of each size and wattage on the machine. Rear and front zones usually differ, so the list is longer than people expect.
- Include the nozzle-end band — it works hardest and fails first.
Sensors
- One spare per length and type used, not per zone: several zones usually share a specification.
- One spare for the zone you have replaced before. Every plant knows which one that is.
Cable and connections
- One extension cable of the correct type and length.
- Plugs, jacks and terminal blocks — cheap, and they stop lines for hours.
Consumables
- Ceramic insulators, sleeving, and heat-resistant protection for leads.
- Thermocouple fittings and clamps.
The test for each item: how long to get it, what the machine loses per hour while it waits, and whether the part is cheap against that number. Where the answer is yes, hold one.
Two rules that make a spare list real:
- Write the part numbers down, and keep the list with the machine. A spare without a number is a spare that gets used and never replaced.
- Replace what you use, immediately. The most common failure of a spare strategy is discovering that it was a one-time purchase.
Thermocouple Products will build a spare schedule from your zone list — band sizes, wattages, voltages, sensor lengths — and quote it as a single item. Most plants find it costs less than two unplanned stoppages.
Where to start
If a zone is misbehaving: compare it with its neighbours, then work the five causes in order — depth and position, sheath conduction, band contact, junction type, cable.
If parts disagree with the display: confirm the reading first, with a handheld thermometer or a replacement sensor at the same point, before touching the tool.
If you are specifying bands for a rebuild: note the barrel outside diameter, band width, voltage and wattage for every zone, and calculate the watt density. That list is the whole specification.
If you are building a spare kit: send the zone list and we will build the schedule.
CTA: Request a Quote → /contact · Call (011) 452-6617 · Email tcprod@mweb.co.za
Related reading:
- The Complete Guide to Heating and Measuring an Injection Moulding Machine
- Band Heaters, Cartridge Heaters and Supercoils: Which One Does Your Machine Actually Need?
- What a Failed Heater or Sensor Is Trying to Tell You
- Temperature Sensor Accuracy: Drift, Calibration and Knowing When to Replace
Related products: Mica Band Heaters · Ceramic Band Heaters · Cartridge Heaters · Supercoil Heaters · Thermocouples · Mineral Insulated Thermocouples · Pt100 RTDs · Extension Cable and Connectors
FAQ schema for this page
Why does my barrel zone not hold temperature? Common causes are a band heater with insufficient wattage for the zone, a failing band, a faulty or badly seated thermocouple, a loose connection, or controller tuning. Compare the misbehaving zone with its neighbours first: the machine, product and controller are common to all zones, so any difference is local to that zone. Check the band’s rating and current draw, verify the sensor reading against a handheld thermometer, and inspect terminals for intermittency.
Why does my barrel thermocouple read low? A consistent, stable reading a few degrees low is usually geometry rather than calibration. A long or heavy sheath protruding into cool workshop air conducts heat away from the measuring junction, so the sensor reads a cooler average than the zone. Insufficient depth, a loose fit in an oversized hole, and a shallow seated sensor have similar effects. A slim mineral insulated sensor in a well-fitted hole with minimal exposed sheath reduces the error.
Should I use a mica or ceramic band heater on my barrel? Mica band heaters are rated to about 480°C at a watt density of 3 to 7 W/cm² and suit the great majority of moulding work economically. Ceramic band heaters are rated continuously to 760°C and their insulation reduces heat loss by roughly 25% to 30%, lowering surface temperature and energy consumption. The barrel’s operating temperature decides which is correct: above about 480°C, mica is the wrong construction rather than a cheaper option.
Why does my barrel zone reading wander or jump? Instability is usually electrical rather than a faulty sensor. A grounded junction is welded to the sheath tip and provides no electrical isolation, which on machines with variable frequency drives and switching heater loads produces earth loops and unstable readings. An ungrounded junction is isolated from the sheath and is the sensible default. Loose terminals, moisture in the connection head and a thermocouple extension cable routed alongside power conductors also cause erratic readings.
What spares should I keep for an injection moulding machine? Hold one band heater of each size and wattage used, including the nozzle-end band that works hardest; one thermocouple per length and type used; one cartridge heater and supercoil for the tool that runs most; a spare extension cable of the correct type; and consumables such as plugs, jacks, terminal blocks, ceramic insulators and lead sleeving. Write the part numbers down, keep the list with the machine and replace items immediately as they are used.